- MECHANIZED TUNNELING & TBM SYSTEMS
Tunnel Belt Conveyor System
- Continuous Transport Capacity of 500 to 5,000 ton/h
- Extendable Lengths Up to Several Kilometers
- Massive Logistical Cost & Traffic Reduction Inside the Tunnel
Tunnel Belt Conveyor System
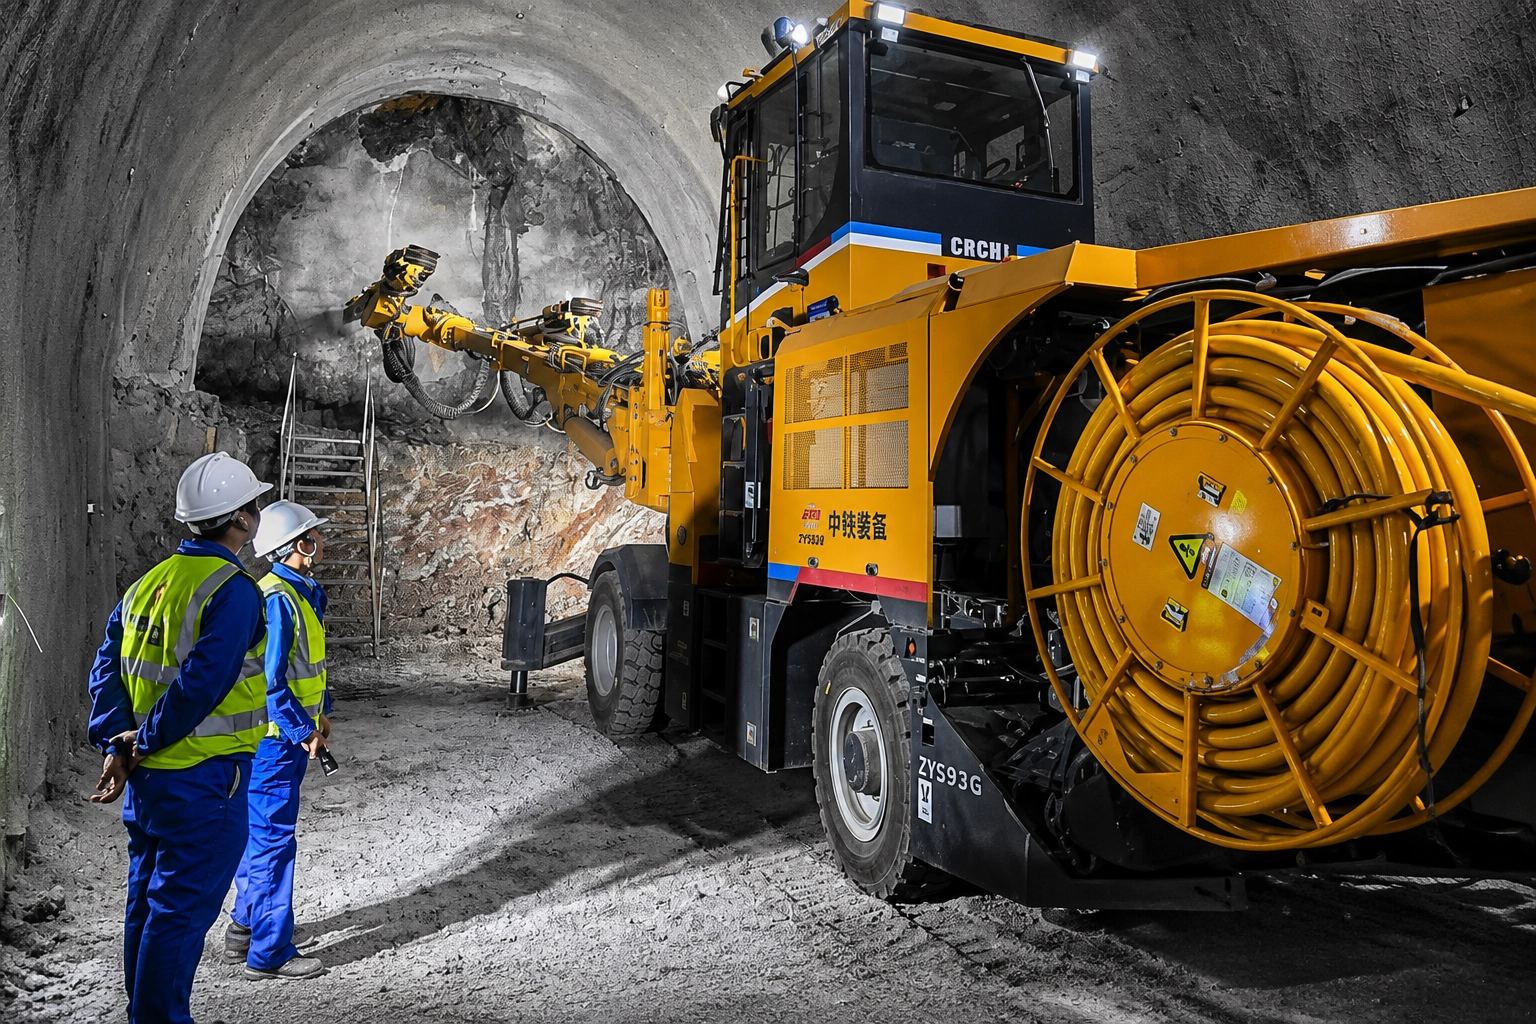
The Tunnel Belt Conveyor System is one of the primary and most efficient material transport solutions in modern mechanized tunneling, designed to continuously transfer excavated muck from the tunnel face to the surface. This advanced logistics system dramatically reduces heavy vehicle traffic inside the tunnel and boosts overall project safety and efficiency.
- Applications
- Continuous Transport of Excavated Material to the Surface
- Supply of Tunnel Construction Materials
- Heavy-Duty Roadheader & TBM Tunneling Projects
- Reducing Internal Tunnel Traffic and Rail Locomotive Dependence
- Working Platforms for 24/7 Operations
- Technical Specifications
| Parameter | Value |
|---|---|
| Transport Capacity | 500 to 5,000 ton/h |
| Belt Width | 600 to 1,800 mm |
| Belt Speed | 1 to 5 m/s |
| System Length | Up to several kilometers |
| Drive Type | Electric motor drive |
- Key Features & Benefits
- Delivers uninterrupted muck removal from 500 up to 5,000 ton/h, perfectly matching the full excavation pace of large-diameter TBMs.
- Scalable belt lengths up to several kilometers with extension segments added progressively as the tunnel drive advances.
- Eliminates heavy truck and locomotive fleets, slashing ventilation load, fuel costs, personnel traffic, and overall project logistics expenses.
- Robust electric motor drives and heavy-duty idler construction guarantee non-stop, failure-free material flow around the clock.